Projection Screen Quality Inspection Checklist for OEM Buyers
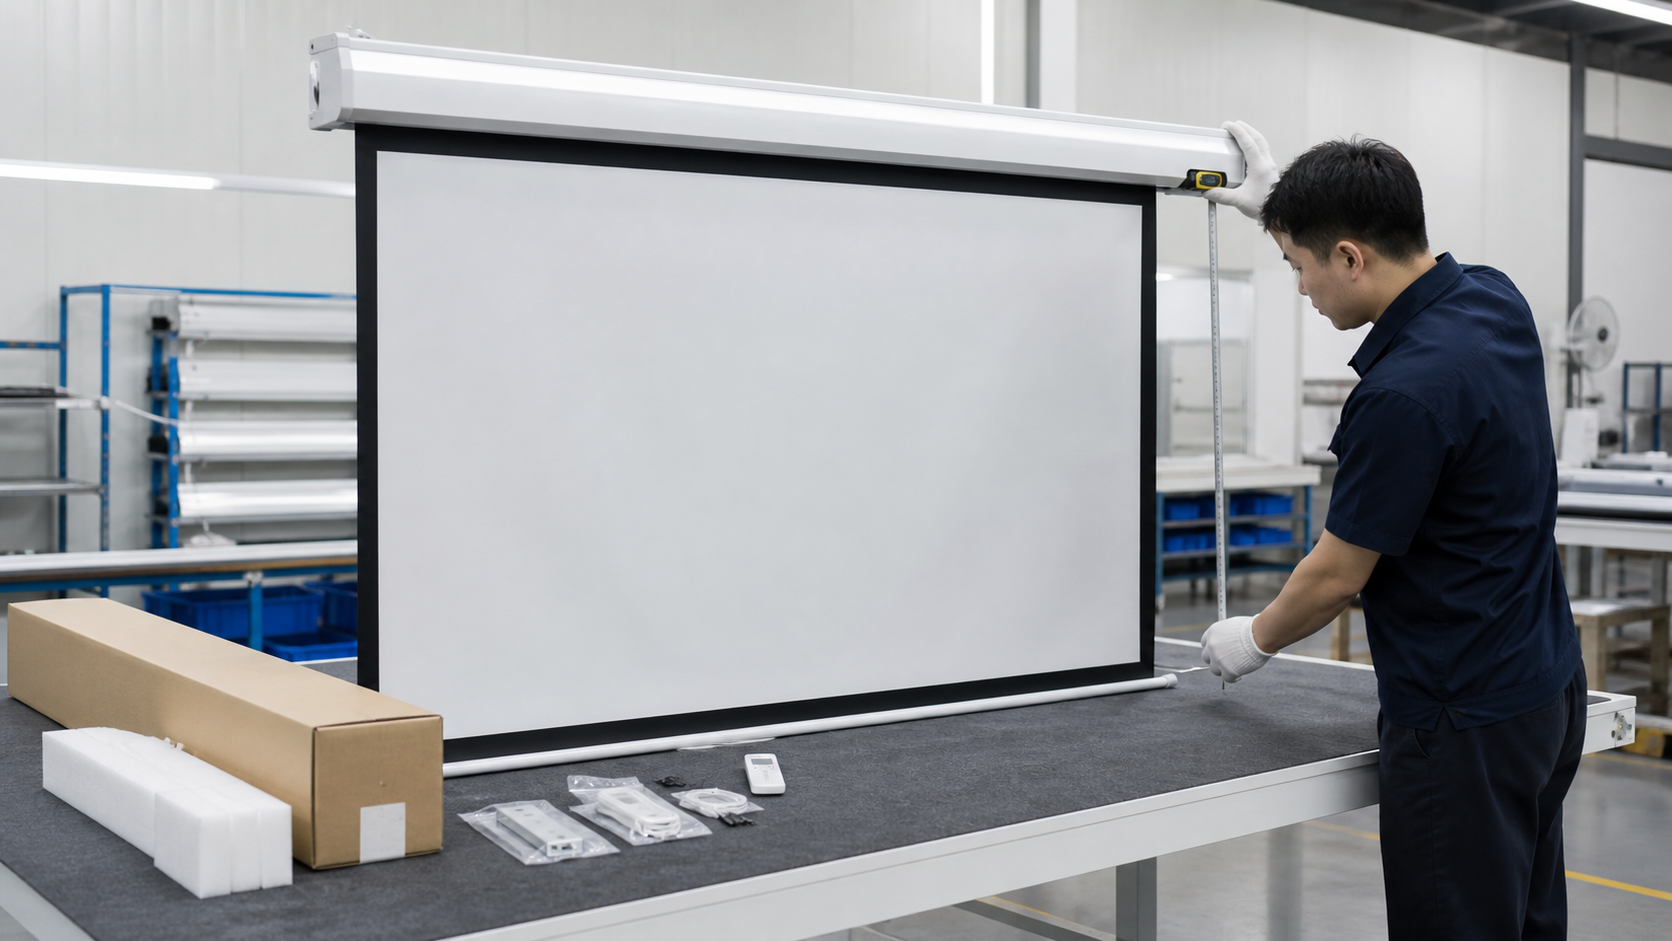
A stage-by-stage inspection guide for OEM buyers checking projection screen identity, dimensions, appearance, operation, accessories, evidence and packaging.
In This Guide
Quick Answer
A projection screen quality inspection should verify the complete delivered configuration against the purchase order, released specification, drawing and approved sample. Checking only whether a motor runs can miss the wrong material, image size, control, accessory set, label revision or packaging.
Use linked inspection stages: incoming material review, first-article approval, in-process checks, finished-product inspection, packing verification and shipment release. Define acceptance criteria before production, record evidence for every failed or conditional item, and use product-specific checks for motorized, tab-tensioned, manual, fixed-frame and portable screens.
Define the Inspection Stages
| Stage | Main purpose | Typical evidence |
|---|---|---|
| Incoming material | Confirm critical surfaces, profiles, housings, motors, controls and packing inputs | Identity record, visual photos and supplier document |
| First-article approval | Verify the first finished configuration before the production run continues | Measurements, operation result, images and disposition |
| In-process inspection | Catch assembly, alignment, tension, wiring or finish problems before final assembly | Process record and corrective-action note |
| Finished-product inspection | Verify identity, dimensions, appearance, operation, accessories and labels | Model-level inspection checklist |
| Packaging inspection | Confirm protection, contents, carton identity and shipping marks | Packing photos, count and carton record |
| Shipment release | Close deviations and reconcile released quantity with order documents | Signed disposition and release record |
The buyer and supplier should agree which stages apply to the order, who performs them, how samples are selected and what evidence will be provided. This guide does not set a universal sampling level, tolerance or defect rate.
Build the Approved Reference Pack
Before inspecting, collect the purchase order, released configuration sheet, drawing, approved sample record, artwork and label files, manual revision, packing list and acceptance criteria. Confirm that these records identify the same model and revision.
The configuration should cover screen type, visible size, aspect ratio, material, housing or frame, mounting, voltage and plug where applicable, motor and controls, accessories, labels, quantity and destination. Use the OEM ordering and document-control guide to prevent one model name from silently covering incompatible configurations.
Where a physical sample is the approval reference, record its sample ID, revision, deviations and approval owner. The sample approval checklist explains how to control that reference before mass production.
Inspect Incoming Material and Components
Incoming material checks focus on critical inputs before defects become embedded in finished products. Confirm the identity and condition of screen surfaces, frame profiles or housings, end caps, bottom bars, brackets, motors, controllers, remotes, fasteners, labels, manuals and packing materials that apply to the order.
For visible surfaces and finished profiles, check contamination, marks, coating or finish consistency, damage and correct orientation. For electrical or control components, verify the released part identity and approved market configuration rather than assuming that similar-looking devices are interchangeable.
Record quarantined or substituted material separately. A substitution should not enter production until its technical, commercial, documentation and inspection effects are reviewed and released.
Complete First-Article Approval
First-article approval verifies one finished configuration before a larger production run proceeds. The first article should be traceable to the production materials, settings, artwork and packing direction intended for the order.
Measure the visible image width and height, aspect ratio, border or extra drop, overall housing or frame dimensions, mounting positions and relevant alignment points against the approved drawing. Record the measurement method and agreed tolerance; do not replace measured values with a nominal catalog size.
Run applicable operation checks, review appearance, verify the supplied controls and accessories, and compare labels and manuals with the released files. Close every difference through correction, an authorized deviation or an updated approved reference. Do not treat an unresolved first article as an automatic production release.
Use a Core Finished-Product Checklist
| Inspection area | What to check | What to record |
|---|---|---|
| Identity | Model, revision, quantity, destination and serial/batch reference where used | Traceable product record |
| Dimensions | Image area, ratio, border/drop, overall size and mounting features | Measured values and method |
| Surface | Marks, contamination, waves, edge curl, texture, orientation and visible uniformity | Photos and viewing conditions |
| Structure | Housing/frame, joints, end caps, brackets, bottom bar and fasteners | Visual and dimensional record |
| Operation | Deployment, retraction, locking, stop positions, tracking and stability | Test result and observed condition |
| Controls | Only the supplied and released interfaces | Control identity and response |
| Accessories | Brackets, cables, remotes, manuals and approved spares | Count against packing list |
| Labels | Model, electrical, barcode, destination and revision fields | Clear label images |
| Packaging | Carton, internal protection, accessory separation and shipping marks | Packing record and photos |
Apply Product-Specific Checks
Motorized and Tab-Tension Screens
For electric projection screens, verify full deployment and retraction, upper and lower stop positions, fabric tracking, bottom-bar alignment, controller response and the released power/control configuration. Record abnormal movement, vibration or sound as an observed condition without applying an unapproved numeric noise limit.
For tab-tension screens, inspect both side cables or cords, tabs, travel path, edge behavior and symmetry. Check that nothing binds or rubs and that the screen is evaluated under agreed settling, projector and viewing conditions. Review the tab-tension surface acceptance guide when defining project-specific flatness evidence.
Manual Screens
For manual projection screens, check pull-down movement, locking positions, controlled retraction where applicable, operating reach, bottom-bar alignment and the condition of the pull ring or operating point. Repeat the approved operating sequence and watch for uncontrolled return, sticking or inconsistent locking.
Do not evaluate a manual mechanism using instructions from a different model. The inspection record should identify the exact unit and operating method supplied.
Fixed-Frame Screens
For fixed-frame screens, verify profile identity, visible dimensions, squareness, corner joints, connectors, mounting hardware and the supplied tensioning system. Assemble an inspection unit when the order's acceptance plan requires it rather than approving only packed profiles.
Inspect the material orientation, perimeter attachment, border or bezel alignment and image plane after correct assembly. Record gaps, twist, joint mismatch or uneven attachment against the approved reference and installation method.
Portable Screens
For portable screens, check case condition, folding frame or support structure, hinges, locks, legs, feet, material attachment, accessory set and packing sequence. Set up the inspection unit on a suitable surface and confirm stability under the intended indoor inspection condition.
Transport handles, bags, cases and small accessories are part of the delivered configuration. Count and photograph them, and confirm that the packed arrangement protects the screen material and structural parts from contact damage.
Review Appearance and Image-Plane Condition
Appearance and image-plane inspection should use documented conditions. Record viewing distance, room light, projector model and geometry where used, image content or test pattern, screen settling time and reference sample. Separate optical artifacts from mechanical waves or installation alignment.
Inspect housing/frame finish, end caps, joints, bottom bar, visible fasteners, labels and the screen surface. On the image plane, look for contamination, handling marks, scratches, texture irregularity, waves, edge curl, uneven tension, visible joints or geometric distortion against the agreed acceptance reference.
Material gain, viewing angle, ALR/CLR/UST behavior and acoustic performance require material-specific evidence. Do not infer those results from appearance alone; use the Screen Materials center and request current model/material confirmation.
Test Operation and Controls Safely
Operate only the released interfaces for the exact model. IR, RF, trigger, dry contact, RS-485 and other integrations are not interchangeable by default. Record controller identity, wiring or connection arrangement, power condition and the result.
For motorized products, complete the agreed cycle and confirm stop positions, travel, tracking and response. Do not alter limit settings or tension adjustments to hide a condition before evidence is captured. If service work is required, follow model-specific approved instructions and record the corrective action and recheck.
The motorized screen commissioning guide can support a project-level record, but the selected controller and motor instructions remain authoritative.
Verify Accessories, Labels and Documents
Count brackets, fasteners, cables, controls, remotes, manuals, tools and approved spare parts against the released packing list. Confirm that accessory labels and model references match the main product.
Check the product label for the fields approved for the supplied configuration and destination. Certification marks or declarations must not be copied from another model. Review available documentation through the certifications and compliance guide and confirm exact scope with the responsible team.
Manual diagrams, parts lists, operating instructions and support contacts must match the hardware in the carton. Record the document revision in the inspection report.
Inspect Packaging Before Shipment
Inspect packaging before the carton is closed and again after packing. Check product wrapping, end and corner protection, separation of accessories from visible surfaces, movement inside the carton, carton identity, barcode and shipping marks. Photograph the packed product and closed carton from useful angles.
Use the projection screen packaging and shipping guide to align protection with the route and receiving process. Do not claim a packaging test level or performance result unless it is supported by a controlled record for the actual package.
Reconcile packed quantity, carton count, model mix and marks with the packing list before shipment release. Transit damage visible at destination should be photographed before the product is moved or unpacked further.
Use Consistent Defect Classification
Define defect classification and disposition before inspection. Useful order-specific statuses include accepted, minor correction, major nonconformance, conditional release and rejected. The parties should define what each status means for the current product and order rather than importing an unexplained generic standard.
Every nonconformance should show the requirement, observed condition, model/lot, clear evidence, owner, corrective action, recheck and final disposition. Conditional release needs written approval and a record of any downstream action. A corrected item should be re-inspected against the same requirement.
Build a Traceable Inspection Report
The inspection report should identify order, product, model, revision, quantity inspected, sample method, date, location, inspector and released reference pack. Include measured values, operation results, images, accessory and label checks, packing evidence, defects, corrective actions and final disposition.
Name evidence files so they can be linked to the order and model. Keep original images and avoid a report that contains only a generic pass stamp. The report should make it possible for a buyer or supplier reviewer to understand what was checked and which configuration was released.
Confirm the Inspection Scope for an MGF Project
For MGF in-ceiling electric screens, record the housing version, visible dimensions, overall length, fixing positions and approved ceiling opening as separate fields. Confirm the supplied controller and accessories against the order. MGF reports motor noise of approximately 30 dB for ceiling screens; any acoustic acceptance criterion needs an agreed motor, load and measurement method.
Use the actual material code and compatible model, and include the installation conditions for a conference-room application.
Provide the configuration, drawing revision, packing requirements and evidence your receiving team needs.
Discuss OEM inspection requirementsFAQ
Is a motor test enough for an electric projection screen?
No. A motor may run while the material, dimensions, controls, accessories, labels or packaging are incorrect. Inspect the complete released configuration.
Should every projection screen be inspected?
Inspection scope and sampling depend on the order, product risk and agreed acceptance plan. Define the method before production; this guide does not prescribe a universal sample level.
What should happen when production differs from the approved sample?
Stop and document the difference. Decide whether to correct the product, authorize a controlled deviation or revise the approved reference before release.
How should screen flatness be inspected?
Agree the screen model, material, setup, settling time, viewing distance, projector geometry, test content and pass condition. Record evidence before changing tension or limits.
Can a factory use its internal QC form?
Yes, when the form covers the exact order and approved criteria and provides useful evidence. A generic passed-QC statement does not replace a model-specific inspection record.
What belongs in a pre-shipment inspection report?
Include order and model identity, reference revision, inspection quantity/method, measurements, appearance, operation, accessories, labels, packaging, photos, defects, corrections and final release disposition.
Request a Model-Specific Inspection Plan
Send the product family, model/configuration, visible size, material, controls, quantity, destination, packaging route and acceptance requirements through MGF Contact. The Factory & Production page provides manufacturing context; exact inspection points, tolerances, sampling and evidence must be agreed for the current order.