Tab-Tension Projection Screen Manufacturing and QC Guide
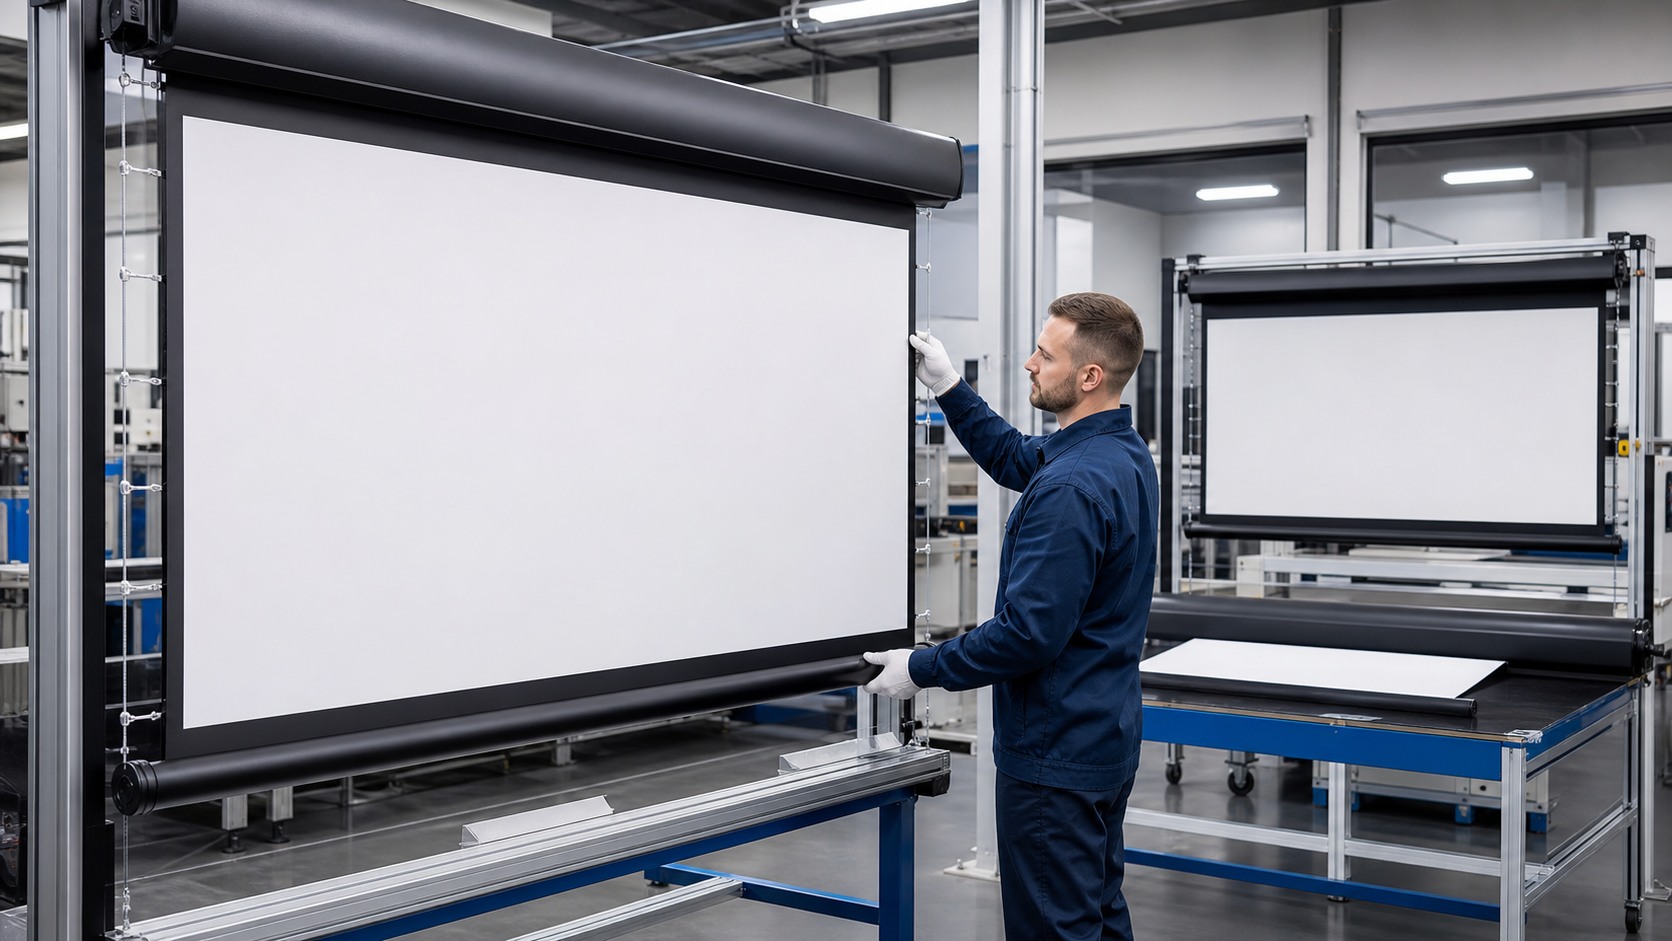
A manufacturing and quality-control guide for buyers reviewing tab-tension material preparation, assembly, limits, flatness evidence and site handoff.
In This Guide
Quick answer
Tab-tension projection screen quality depends on the complete system: fabric, side tensioning, bottom bar, housing, motor, limit settings, installation geometry and inspection method. Buyers evaluating an OEM supplier should ask how each stage is controlled and how the approved sample is matched in production.
The goal is not to promise a perfectly flat surface under every condition. The goal is to define the configuration, installation requirements, acceptance criteria and records that make quality repeatable.
Keep the inspection chain within one identified assembly
For a sample record, use one batch identity to connect material preparation, side-tension components, bottom-bar assembly and complete-screen inspection. Each photo needs the same assembly/reference, inspection stage and conditions. The record below is blank; it is not a fabricated factory pass report.
| Factory record | Site record |
|---|---|
| Specified material/components and assembly against the controlled BOM | Installed support, level, clearance and environment |
| Observed travel/limits and appearance under recorded factory conditions | Actual projector/lens, full image, intended seats and room lighting |
| Agreed inspection method, defect/retest and release signature | Room-specific acceptance, control integration and unresolved issues |
Download tab-tension batch evidence record (CSV). Blank fields are for project records; completing the form does not approve an installation or product combination.
Compare the tab-tension product direction with its exact model records, then use the site acceptance checklist. A factory inspection does not prove absolute flatness in every installation or projector geometry.
Send model/batch, drawing revision, observations, installation conditions and inspection photos. Request a Tab-Tension QC Review.
Manufacturing and QC checkpoints
| Stage | What to control | Typical evidence |
|---|---|---|
| Material receipt | Surface, roll condition and identification | Incoming record |
| Cutting/preparation | Image size, border and orientation | Dimension sheet |
| Tension system | Tabs, cables, bottom bar and attachment | Assembly check |
| Housing/frame | Alignment, brackets and finish | Visual record |
| Motor/controls | Motor, limits and confirmed interface | Functional test |
| Deployment | Tracking, waves and stop positions | Cycle log |
| Final inspection | Surface, dimensions and accessories | Inspection report |
| Packing | Protection, labels and carton | Packing record |
1. Define what “tab-tension” means for the project
State whether the screen is wall-mounted, ceiling-mounted or recessed, and identify the intended screen material, visible image dimensions, ratio, black border, extra drop and control method. Link to the tab-tension product family and the tab-tensioned vs non-tensioned comparison for the selection context.
Selection and production QC are different jobs. Use the screen waves and tab-tension troubleshooting guide to distinguish service symptoms from manufacturing acceptance questions.
2. Control material preparation
Record material name or code, roll direction, image-area dimensions, border and any required sample reference. Inspect the surface for marks, contamination, texture variation and visible defects before assembly. Keep the material identity linked to the model and order revision.
Do not infer gain, viewing angle or UST compatibility from the word “tab-tension.” Those properties belong to the selected surface and must be confirmed by controlled product information or sample evaluation.
3. Assemble the tension system consistently
The side tabs, cables, bottom bar and housing must be assembled according to the approved design. Check attachment points, symmetry, cable routing and mechanical clearance. For a motorized unit, verify that the screen can deploy and retract without abnormal resistance or contact.
4. Set and test limits
Upper and lower stop positions should be set and checked for the exact motor and control configuration. Run a complete cycle and record tracking, bottom-bar alignment, unusual noise and remote or wall-switch response. Use the limit-setting and commissioning guide for the test sequence.
5. Inspect installed flatness realistically
Inspect the screen after installation at the intended viewing distance and room conditions. Check edge waves, diagonal tension, bottom-bar alignment and visible surface behavior. Installation level, temperature, storage and tension condition can influence the result; a factory inspection cannot replace correct site installation.
Make inspection photographs traceable
Label each evidence set with the order or inspection reference, configuration, date and drawing revision. Keep an overall view before close-ups, retain originals and identify annotated copies. State what each image supports: identity, visible condition, a functional observation under recorded conditions, or packaging. A grid photograph alone is not a calibrated flatness measurement, and sample photographs do not prove that every unit was tested.
6. Match production to the approved sample
The approved sample record should identify fabric, dimensions, housing, motor, control, accessories and packaging. If any of these change, issue a revision and decide whether a new sample or corrective action is required.
Connect the production record to the projection screen quality inspection checklist and confirm the applicable process with Factory & Production.
7. Connect QC to site acceptance
Give the installer the final dimensions, brackets, control notes, service clearances and commissioning record. The motorized screen commissioning guide can link factory inspection with field verification.
FAQ
Does tab-tension guarantee a flat screen in every room?
No. The result also depends on material, installation level, tension condition, temperature, storage and projector setup. Confirm the application and acceptance conditions.
What should an OEM buyer ask the factory to test?
Ask for dimensions, surface condition, tension assembly, deployment, retraction, limits, controls, accessories and packaging checks relevant to the exact model.
Is tab-tension only for motorized screens?
Tab-tension structures are commonly associated with motorized systems, but the correct product choice depends on the manufacturer’s available configurations and project requirements.
Should QC numbers be published on the website?
Only if they are current, model-specific and supported by controlled records. Otherwise describe the inspection process without inventing performance figures.
Request a tab-tension QC discussion
Send the product type, size, material, installation, control method, quantity and destination through MGF Contact. MGF can confirm applicable structure and inspection documents for the quoted configuration.